About Us
About Us – Reva Enterprise
We Manufacture CBS-X and various Optical Brightening agents
Reva Enterprise
REVA Enterprise is committed to delivering high-quality products that meet the evolving needs of industrial applications. With a strong focus on quality, reliability, and consistency, we strive to provide solutions that support efficient operations and long-term customer satisfaction.
At REVA Enterprise, quality is never compromised. We emphasize careful product selection, quality-focused processes, and dependable service to ensure our customers receive products they can trust. Our commitment to excellence drives us to build lasting relationships and deliver value through every product we offer.


Our Approach
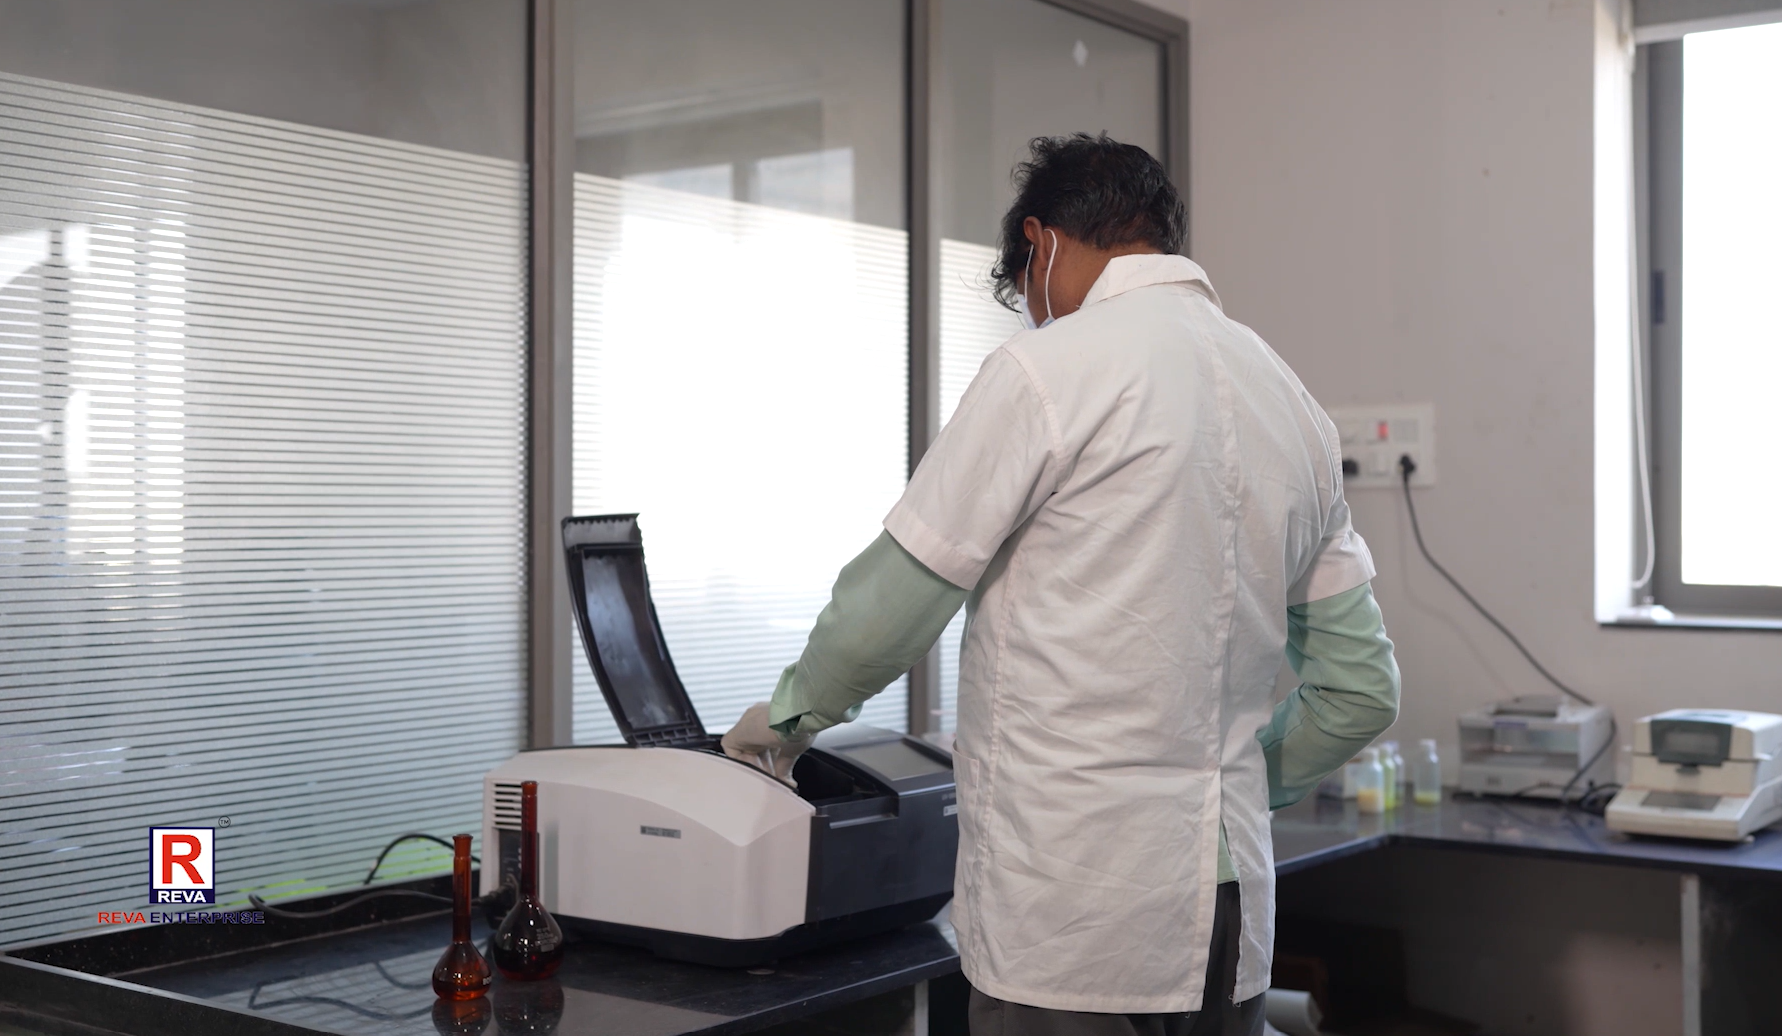
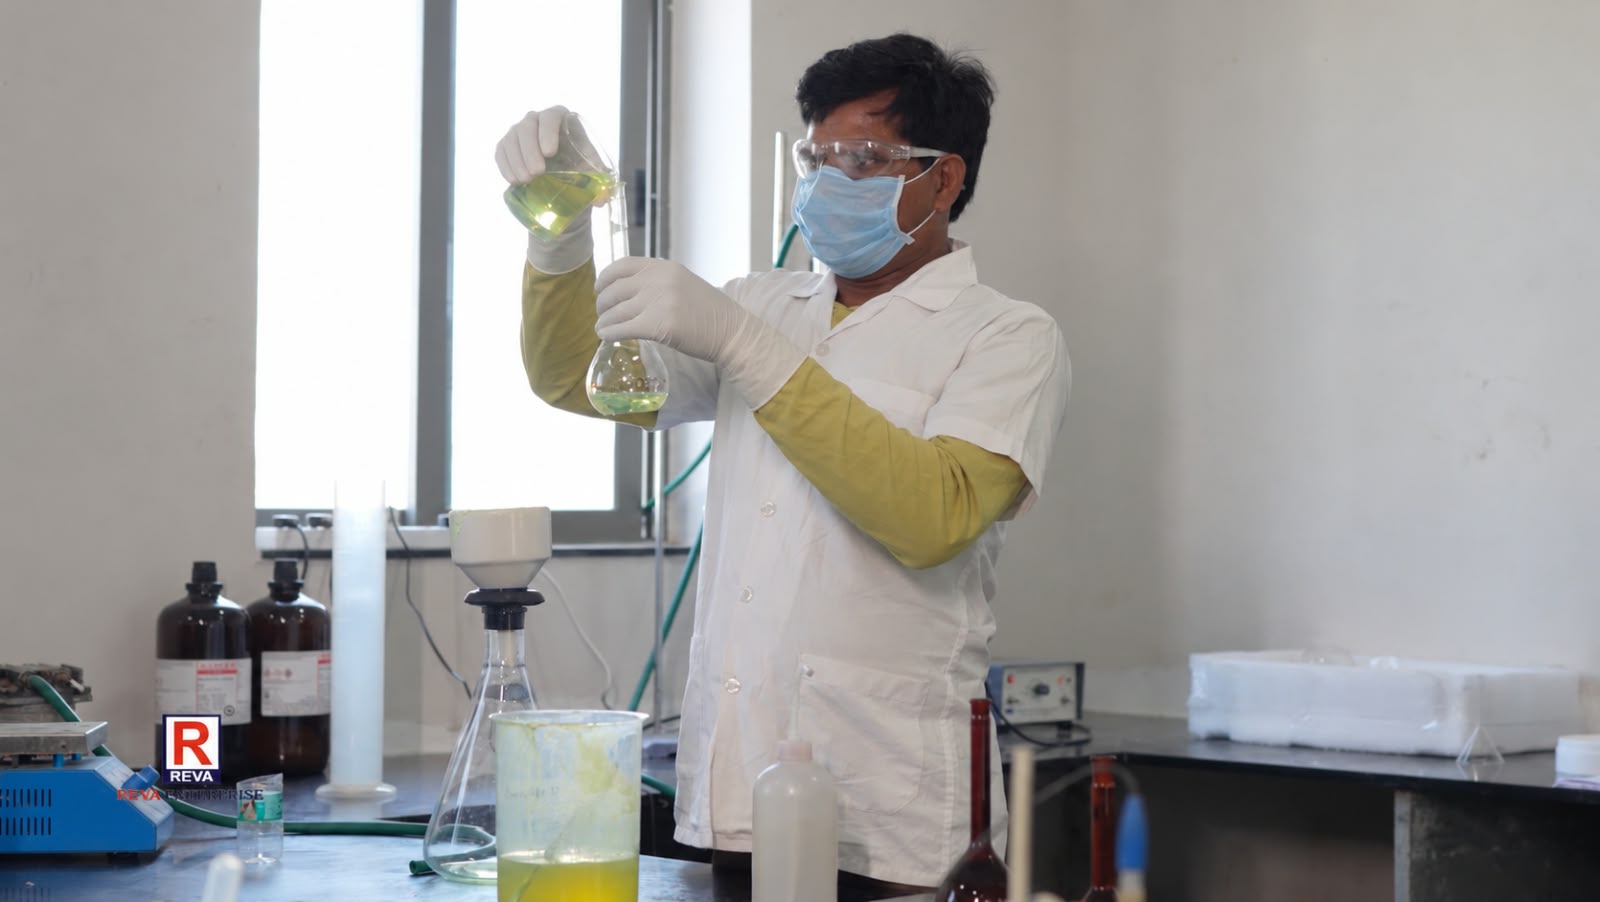
By analyzing current market demand and leveraging technical expertise, Reva Enterprise develops specialized chemical compositions to meet customer requirements. The company emphasizes consistent product quality, adherence to industry standards, and timely delivery.
With experienced technical professionals and dedicated quality analysts, Reva Enterprise focuses on maintaining product quality through established quality-control processes. Its products serve manufacturers that use specialty chemicals as raw materials, as well as industrial and domestic customers across India and international markets.
Reva Enterprise
Our Mission
To deliver high-performance optical brightening agents and specialty chemical solutions through continuous innovation, strict quality control, reliable service, and a commitment to customer satisfaction and sustainable industrial growth.
Reva Enterprise
Our Vision
Reva Enterprise
Why Choose Reva Enterprise?
Consistent Product Quality
We focus on quality control and product evaluation to support reliable performance across industrial applications.
Advanced Manufacturing
Our manufacturing capabilities and process-focused approach help maintain precision, efficiency, and product consistency.
Research & Development
We continuously work to improve our products and develop solutions that address changing industry requirements.
Industry-Specific Solutions
Our product portfolio serves the detergent, paper, and textile industries, with grades designed for different application needs.