Introduction
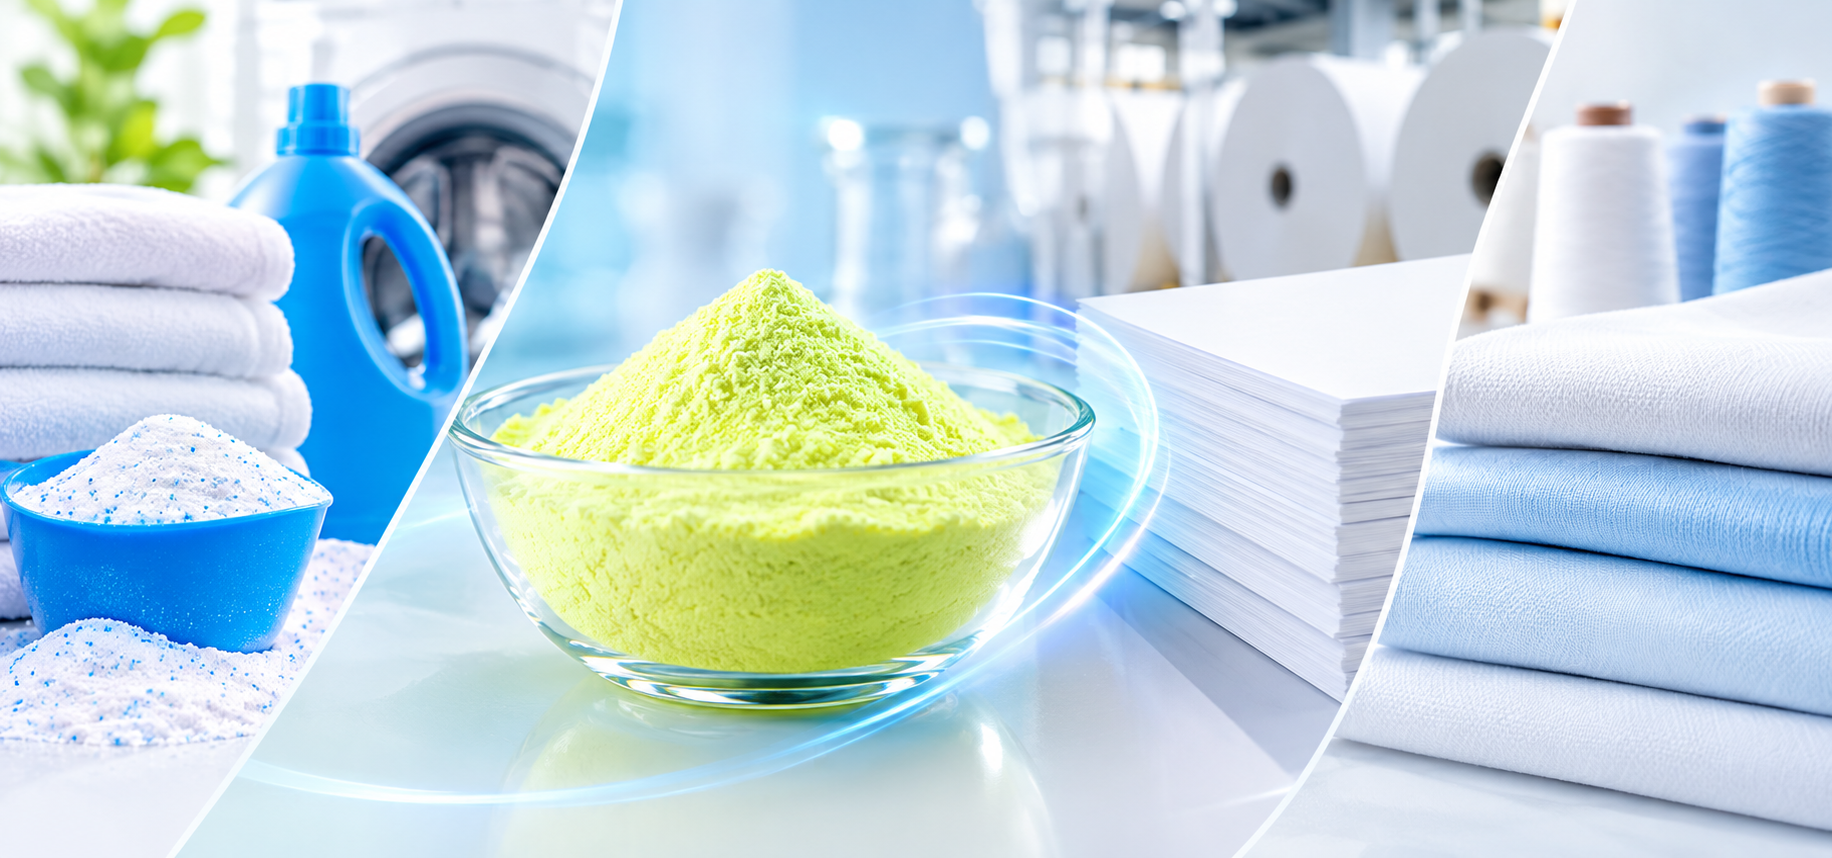
Whiteness and brightness play an important role in the appearance and quality of many industrial products. From laundry detergents and paper products to textile fabrics, manufacturers use specialized chemicals to achieve the desired visual finish. Optical Brightening Agents (OBAs), also known as fluorescent whitening agents, are widely used to enhance the perceived whiteness and brightness of compatible materials.
At Reva Enterprise, we provide optical brightening solutions for industrial applications, helping manufacturers identify products suited to their processing requirements.
What Are Optical Brightening Agents?
Optical Brightening Agents are specialty chemicals that absorb ultraviolet light and emit part of that energy as visible blue light. This optical effect helps reduce the appearance of yellowish tones, making compatible materials appear brighter and whiter.
Unlike conventional whitening methods that rely only on removing impurities or adding white pigments, OBAs work through fluorescence. Their effectiveness depends on the chemical grade, substrate, dosage, and processing conditions.
Key Benefits of Optical Brightening Agents
1. Enhanced Whiteness and Brightness
OBAs help improve the visual whiteness of suitable materials, supporting a cleaner and brighter appearance in finished products.
2. Improved Product Appearance
In applications such as laundry detergents, paper, and textiles, optical brighteners can contribute to the desired appearance and perceived product quality.
3. Application-Specific Solutions
Different optical brightener grades are designed for different industrial processes. Selecting a suitable grade helps manufacturers meet their specific performance requirements.
4. Compatibility with Industrial Processes
Depending on their chemistry, certain OBAs can be incorporated into powder, liquid, and other compatible formulations. The appropriate product should be selected according to process conditions.
Applications of Optical Brightening Agents
Optical Brighteners for the Detergent Industry
Optical brightening agents are used in washing powders, laundry detergents, and compatible soap formulations to improve the perceived whiteness of washed fabrics. The selected grade must be suitable for the detergent formulation and its alkaline conditions.
Reva Enterprise offers detergent-industry products, including REVA™ CBS-X Powder, designed for optical brightening applications in soaps and detergents.
Optical Brighteners for the Paper Industry
In paper manufacturing, optical brighteners can help improve the perceived whiteness and brightness of suitable paper grades. Their performance depends on factors such as paper composition, furnish chemistry, application method, and production conditions.
Selecting the correct grade and dosage is important for achieving consistent results in the intended paper-processing system.
Optical Brighteners for the Textile Industry
In textile processing, optical brighteners are used to enhance the visual whiteness of compatible fibres and fabrics. The appropriate grade depends on the fibre type, treatment method, bath chemistry, and required finished appearance.
Laboratory trials help determine the suitability and dosage of an optical brightener for a particular textile application.
How to Choose the Right Optical Brightening Agent
Choosing an appropriate optical brightener requires consideration of several factors:
- Industry and application: Identify whether the product is intended for detergent, paper, or textile processing.
- Chemical compatibility: Check compatibility with other ingredients, processing chemicals, and the substrate.
- Physical form: Select a powder or liquid grade according to handling and manufacturing requirements.
- Performance requirements: Consider the required whiteness, brightness, and process conditions.
- Technical specifications: Review the product’s approved technical data sheet (TDS), including active content, pH, stability, and recommended dosage.
Conducting application trials before full-scale production can help confirm performance and process compatibility.
Why Choose Reva Enterprise?
Reva Enterprise supplies optical brightening agents and specialty chemical solutions for the detergent, paper, and textile industries. Our product portfolio includes different grades intended to address varied industrial processing requirements.
We focus on product suitability, consistent quality, and customer support to help manufacturers evaluate appropriate brightening solutions for their applications.
Conclusion
Optical Brightening Agents are valuable specialty chemicals for enhancing the perceived whiteness and brightness of compatible detergent, paper, and textile products. Achieving the desired result depends on selecting the correct grade, understanding the application conditions, and using an appropriate dosage.
Reva Enterprise offers optical brightening solutions for industrial manufacturers seeking products suited to their processing needs.
Looking for an optical brightening solution for your application? Contact Reva Enterprise to discuss your product requirements.
